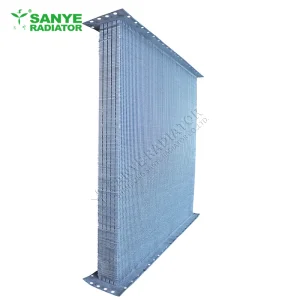
Explore our premium range of high-efficiency brazed aluminum and heavy-duty automotive cooling cores designed for extreme durability and optimal thermal performance.
Positioned at the intersection of rugged topography and burgeoning agricultural and infrastructural development, Ngozi requires specialized engineering solutions to maintain mechanical longevity under harsh operating conditions.
Driven by heavy commercial transport, regional logistics, and agricultural processing machinery, Ngozi’s industrial landscape demands reliable thermal solutions that prevent engine thermal breakdown and maximize equipment uptime in high-ambient-temperature environments.
Our manufacturing utilizes state-of-the-art vacuum brazing technology, high-grade aluminum alloys, and stringent pressure-impulse testing. This ensures superior resistance against thermal fatigue, vibration stress, and corrosive operational settings worldwide.
Backed by ISO/TS 16949 international quality standards, we provide tailored export logistics, customs compliance assistance, and robust technical documentation to ensure seamless supply chain integration for distributors and fleet operators in Ngozi.
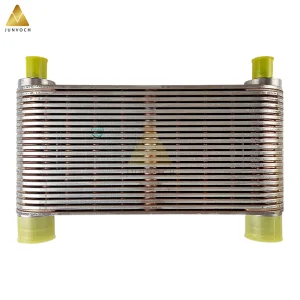
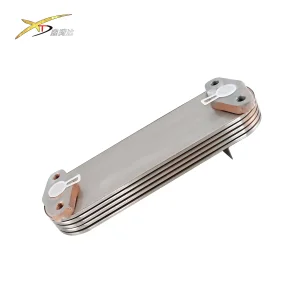
From high-altitude freight transport to heavy-duty mining and agricultural tractors, our oil cooler cores deliver optimized heat dissipation across multiple demanding sectors.
Long-haul trucks operating through challenging regional terrains require consistent engine oil temperature regulation to prevent viscosity breakdown and prolong engine lifespan.
Tractors and processing equipment in agricultural hubs benefit from robust brass and aluminum cores designed to resist clogging from dust and operate efficiently during peak seasonal workloads.
Excavators and construction generators equipped with Cummins, Caterpillar, and Komatsu powerplants rely on our high-performance oil cooler cores to endure continuous heavy-load operations.
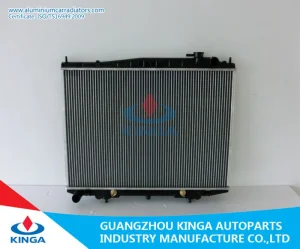
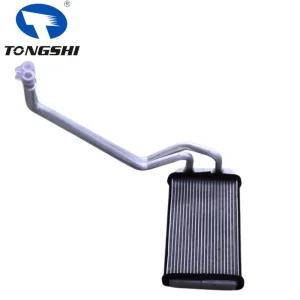
Browse our extensive inventory of automotive radiator cores, heater cores, and specialized machinery oil coolers manufactured for global export and local distribution.
Expert insights regarding our automotive oil cooler cores, export procedures, and compatibility for Ngozi clients.
Established in 2007, Zhejiang Rock Auto Co., Ltd. has been a leading manufacturer, exporter, and supplier of high-performance auto cooling system components. We specialize in producing a wide range of automotive cooling solutions, including radiator tubes, intercooler tubes, oil cooler tubes, as well as radiators, intercoolers, and oil coolers.

With more than 15 years of industry experience, Zhejiang Rock Auto has earned a reputation as a pioneer in the design and manufacturing of aluminum-based cooling products. We are committed to providing high-quality, cost-effective, and innovative solutions that meet the rigorous demands of our global customers. Our products are widely used in automobile, heavy industry, shipbuilding, sugar processing, packaging, navigation, molds, and other specialized applications.
At Zhejiang Rock Auto, we pride ourselves on our dedication to excellence and client satisfaction. We approach every project with a well-defined strategy, from initial design to final production, ensuring that our customers receive only the best in terms of quality and performance. Our team continuously works to enhance the efficiency of our products, driven by extensive research and development (R&D) efforts. Through continuous innovation, we develop solutions that meet the evolving needs of the market.
Our R&D unit is the cornerstone of our business, conducting detailed research and surveys to improve the performance and durability of our products. This commitment to innovation allows us to design new products with superior functionality, tailored to the specific needs of our clients. Additionally, we actively explore new applications for our cooling solutions, ensuring we remain at the forefront of the industry.
We are proud to be ISO/TS 16949 certified, and our state-of-the-art manufacturing facility is equipped with advanced technologies, including Brazing Furnaces, Fin Machines, and Core Assembly Machines. Our skilled and experienced team is proficient in all aspects of the manufacturing process, from design to final quality checks, ensuring that every product meets the highest standards.
As a customer-centric company, Zhejiang Rock Auto Co., Ltd. aims to achieve maximum customer satisfaction. We uphold the highest ethical standards in all aspects of our business and are committed to continuous improvement. Our relentless pursuit of excellence has enabled us to expand our presence globally, making us a trusted partner for businesses around the world.
To deliver high-quality and cost-effective cooling solutions that not only meet but exceed customer expectations, while fostering a culture of innovation and sustainability.
To be a global leader in the auto parts industry, recognized for our advanced technologies, outstanding customer service, and environmental stewardship.
 Rock Auto